Pulse Counting in Automatic Packaging Machines: Distinguishing Double Counting Errors from Missing Real Products
Double counting means a single product passes by a sensor once, but the counter registers two or more pulses. Conversely, a missing product error means the machine completes a full packaging cycle, but the package contains no goods inside. These two faults present opposite symptoms on the counter, and their technical root causes lie on completely different sides: sensors versus mechanics. This is where most confusion arises when first dealing with automatic packaging equipment. Many operators assume a wrong count indicates a faulty sensor, whereas in most cases, missing products stem from upstream feeding stages, entirely unrelated to the counting sensor.
Why Sensors Register Double Pulses for a Single Product
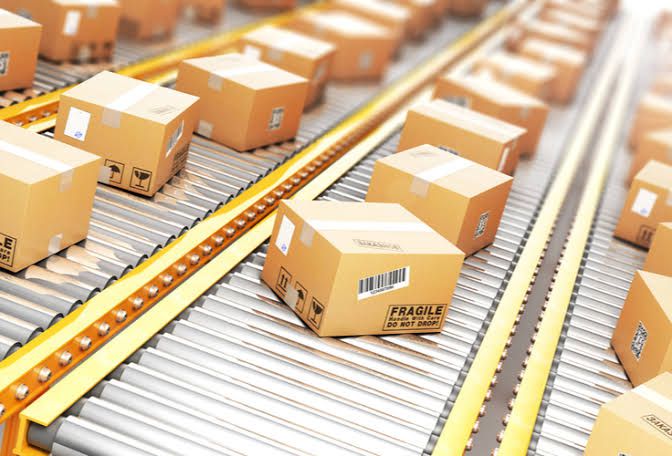
The most common cause is mechanical vibration. Conveyor jerks at joint connections, or packaging cutters creating vibrations that transmit back to the sensor bracket, cause the signal to switch rapidly on and off within a very short timeframe—even as only one product passes by.
Product surface characteristics also play a major role. Glossy products with light-reflecting films can easily trigger a photoelectric sensor twice during a single pass. Products with uneven shapes, holes, or surface grooves create a similar effect as the beam cuts across alternating high and low features. An often-overlooked factor is dust or grease accumulation on the sensor lens. A thin layer of grime makes the reflected signal unstable, generating small noise pulses interspersed between genuine counts.
Why Machines Complete Cycles Without Real Products in Packages
This scenario is virtually unrelated to the counting sensor at the packaging station. The issue typically lies in upstream feeding equipment—such as jammed bowl feeders or bowl vibrators, temporary material depletion, or products clumping together in prior steps—leaving an empty space on the conveyor belt.
You may also be interested in:
Signs of Bearing Wear Through Rotational Speed Fluctuations
The sensor at the packaging station functions correctly; there is simply nothing present to detect at the exact moment the sealing mechanism actuates. This explains why relying solely on a single sensor at the packaging point is insufficient to catch this error.
Distinguishing the Two Errors by Symptom Without Disassembling the Machine
The quickest approach is comparing the displayed count on the screen against the actual quantity inside finished packages. If the recorded count exceeds the real item count, it is almost certainly double counting, pointing to sensor issues or mechanical vibration. If the count matches or is lower but packages are empty, it indicates missing real products, usually originating from feeding stages.
Another quick check is observing error frequency relative to machine speed. Double counting typically increases noticeably at high operating speeds and drops during slow-speed testing. Missing real products depend far less on speed, often correlating with near-empty feed hoppers or localized product jams.
How PLCs Filter False Pulses to Eliminate Double Counting
The most common method is programming a noise filter—known as debounce time—directly in the PLC logic. When the sensor changes state, the PLC does not register a product immediately; instead, it waits for the signal to remain stable for a few to several dozen milliseconds depending on conveyor speed before incrementing the counter by one. Noise pulses caused by vibration are usually too brief to sustain stability across this window and are automatically discarded.
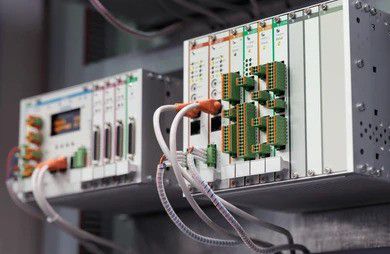
A second approach is establishing a lockout time after each registered count. Based on known conveyor speeds, engineers calculate the minimum time gap between two consecutive products. The PLC then temporarily ignores further incoming pulses from that sensor for a short period following a valid count. For products with glossy surfaces causing multiple reflections, switching to background suppression (BGS) sensors is recommended, as they distinguish real products from background light reflected off the conveyor belt.
Detecting Missing Real Products Using Encoder Synchronization
The most reliable solution involves deploying two sensors at different locations: one at the feed chute to count incoming items, and another directly before the sealing mechanism to confirm actual product presence at the precise packaging moment. If the machine reaches the sealing stage and the second sensor detects nothing, the PLC immediately identifies a missing product fault and triggers an alarm or reject mechanism.
A more rigorous method synchronizes product counting with main shaft encoder pulses. Each shaft rotation corresponds to a fixed number of encoder pulses, requiring an accompanying product sensor pulse within that window. If a full cycle completes without detecting the corresponding product pulse, the system immediately flags a missing product error without waiting for end-of-line checkweighers to detect it.
To capture high-frequency pulses from optical sensors on fast packaging lines, explore pulse counters with high-speed input capabilities in the Tachometers and Pulse Counters catalog at EMIN.