These two parameters frequently appear in technical documentation for industrial, anti-corrosion, and fire-retardant coatings; although they differ by only a few characters, their meanings and contexts of use are entirely distinct. A correct understanding helps control paint consumption from the outset, minimizes the need for rework, and avoids unnecessary costs.
Freshly applied paint and dried paint never look the same
When observing a freshly spray-painted surface, the coating appears thick and glossy, effectively concealing the underlying material. Since the surface retains its shape after hours or even days, one might easily assume the thickness remains unchanged.
However, the solvent within the paint continuously evaporates during the curing process. The final coating consists only of the solid components adhering to the structure's surface; consequently, the thickness after drying is always less than the thickness immediately after application.
This gives rise to two distinct concepts:
- WFT (Wet Film Thickness): The thickness of the paint film measured immediately after spraying or brushing.
- DFT (Dry Film Thickness): The thickness of the paint film measured after the coating has fully cured.
Simply put, while WFT reflects the amount of paint present on the surface, DFT is the value that determines the coating's protective capability.
Why is acceptance testing always based on DFT instead of WFT?
During application, technicians typically monitor the Wet Film Thickness (WFT) to verify whether the paint quantity meets requirements. If the coating is too thin, more can be applied while the paint is still wet; if it is too thick, adjustments can easily be made before material is wasted.
Once the project is complete, WFT is no longer significant. Project owners and supervisors are primarily concerned with the thickness of the remaining coating after the solvent has fully evaporated. This is the actual layer that protects the structure against corrosion, chemicals, or high temperatures.
Standards such as ISO 19840, ASTM D7091, and SSPC-PA 2 all utilize Dry Film Thickness (DFT) as the basis for evaluating coating quality.
If you are working on structural steel or intumescent coating projects, you may wish to consult the article Latest Standards for Intumescent Coating Thickness on Structural Steel (DFT, WFT & Acceptance Procedures to gain a clear understanding of measurement point distribution, evaluation criteria, and acceptance documentation requirements.
How is the DFT calculated from the WFT?
Each type of paint has a different volume solids content. After the solvent evaporates, only the remaining solids form the protective coating.
A commonly used formula is:
DFT = WFT × Volume solids content
For example, consider a type of paint with a solids content of 60%.
If the Wet Film Thickness (WFT) measures 200 μm, the Dry Film Thickness (DFT) will be only about 120 μm after complete drying.
This discrepancy explains why, on many projects, the paint application might appear sufficient, yet final inspection measurements reveal a shortfall of several tens of micrometers compared to the design specifications.
Measuring WFT or DFT depends on the specific stage of the work
When the goal is to control the application process, WFT is the primary parameter to monitor. By detecting a substandard coating layer early, the applicator can immediately adjust the paint volume or the number of spray passes.
DFT becomes a meaningful value only after the coating has fully cured. All acceptance documentation, as well as assessments of the coating's service life and corrosion resistance, are based on this figure. This is why many applicators measure both parameters rather than focusing on a single result.
Which gauge is suitable for measuring DFT?
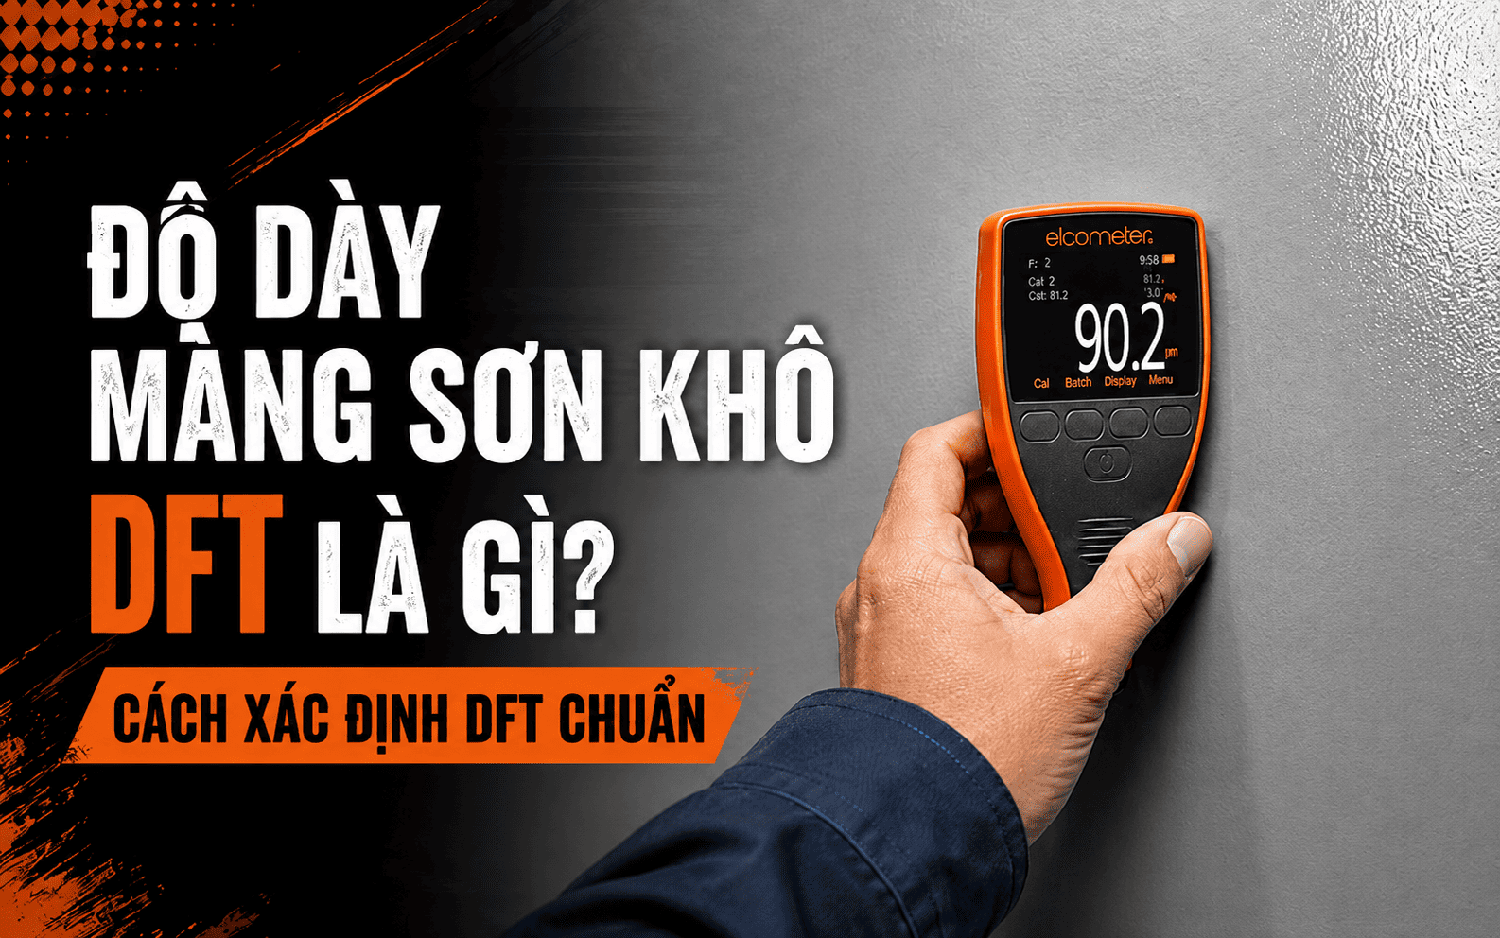
Once the paint has fully cured, wet film thickness gauges are largely ineffective. At this stage, the focus shifts to coating thickness gauges that utilize magnetic induction or eddy current principles to take direct measurements on steel and non-ferrous metal substrates.
Some commonly used devices include:
- DeFelsko PosiTector 6000: Features interchangeable probes, making it suitable for applications ranging from structural steel and storage tanks to heavy-duty thick coatings.
- DeFelsko PosiTest DFTF: A compact, lightweight option ideal for rapid on-site inspections.
- Elcometer 456: A well-known model in the industrial coating sector, valued for its data logging and statistical analysis capabilities, as well as its compliance with numerous international standards.
Understanding these distinctions helps prevent issues such as under-coating, over-coating, or the need for rework due to discrepancies of just a few dozen micrometers. When verifying coating quality against technical standards, selecting the appropriate gauge and measuring at the right time yields far more reliable results than relying on visual inspection alone.